Applications
How to Estimate Self-Loading Concrete Mixer Output per Hour and per Day
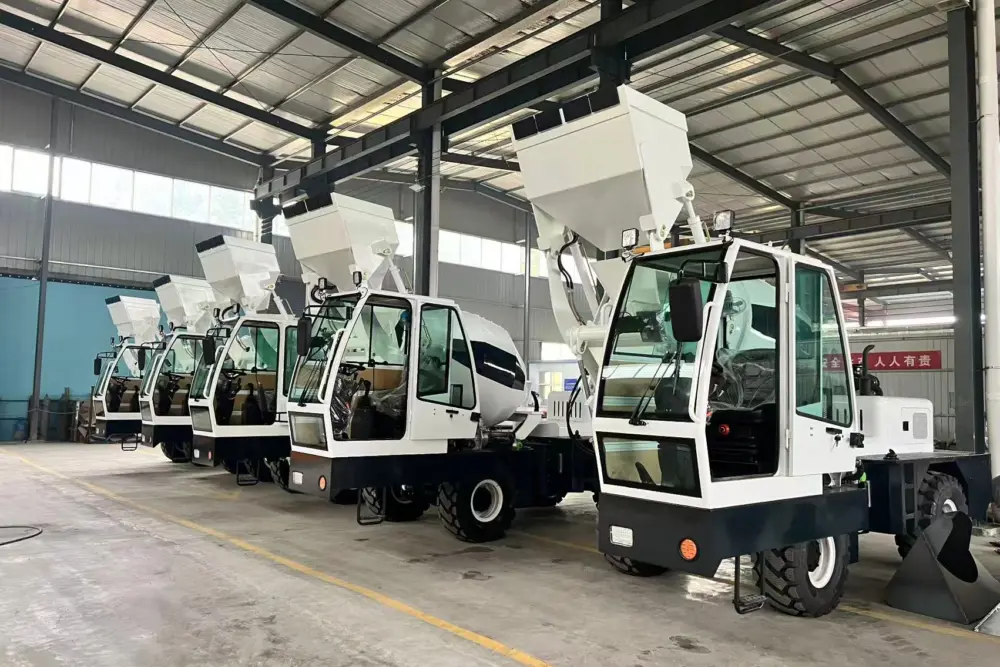
Estimating self-loading concrete mixer output requires two inputs: confirmed concrete yield per batch and a realistic number of complete cycles in the available working time. Multiplying a drum-capacity label by a brochure cycle rate can produce a misleading result.
This guide provides a transparent calculation method for RB1600 and RB2500 and explains why RB4000 output remains unresolved. The examples are planning arithmetic, not guaranteed productivity.
The Core Output Formula
Estimated concrete output = concrete yield per batch × completed batches.
For an hourly estimate, multiply yield by realistic batches per hour. For a shift estimate, either multiply hourly output by productive hours or count expected complete cycles across the shift. Keep every assumption visible so it can be corrected after a site trial.
Use Yield, Not Drum Capacity
RB1600 has 1.6 m³ confirmed yield and a 2.5 m³ drum. RB2500 has 2.5 m³ yield and a 4.5 m³ drum. RB4000 has a 4 m³ drum but no confirmed yield. Only the yield values belong in the output formula.
If a quotation says only “capacity,” ask for the definition. Mixing capacity, geometric volume, discharge capacity and concrete yield may describe different measurements.
Understand “Up to Four Batches per Hour”
RB1600 and RB2500 list up to four batches per hour. The phrase describes a maximum listed rate, not a promise for every jobsite. A full cycle includes more than drum mixing:
- Positioning at material stockpiles
- Loading ingredients
- Adding water and following the required mix procedure
- Mixing
- Travelling to the placement point
- Discharging
- Returning and completing necessary cleaning or checks
Any queue, long route, difficult access or material interruption changes completed cycles.
Calculate the Published Arithmetic Ceiling
RB1600 example
1.6 m³ per batch × 4 batches per hour = 6.4 m³ per hour. This is the arithmetic result at the listed upper batch rate.
RB2500 example
2.5 m³ per batch × 4 batches per hour = 10 m³ per hour. Again, it is an upper-rate calculation rather than a guaranteed result.
RB4000
No supported calculation can be published because concrete yield and batches per hour are not confirmed. Drum capacity and drum speed do not provide the missing values.
Build a Realistic Cycle-Time Estimate
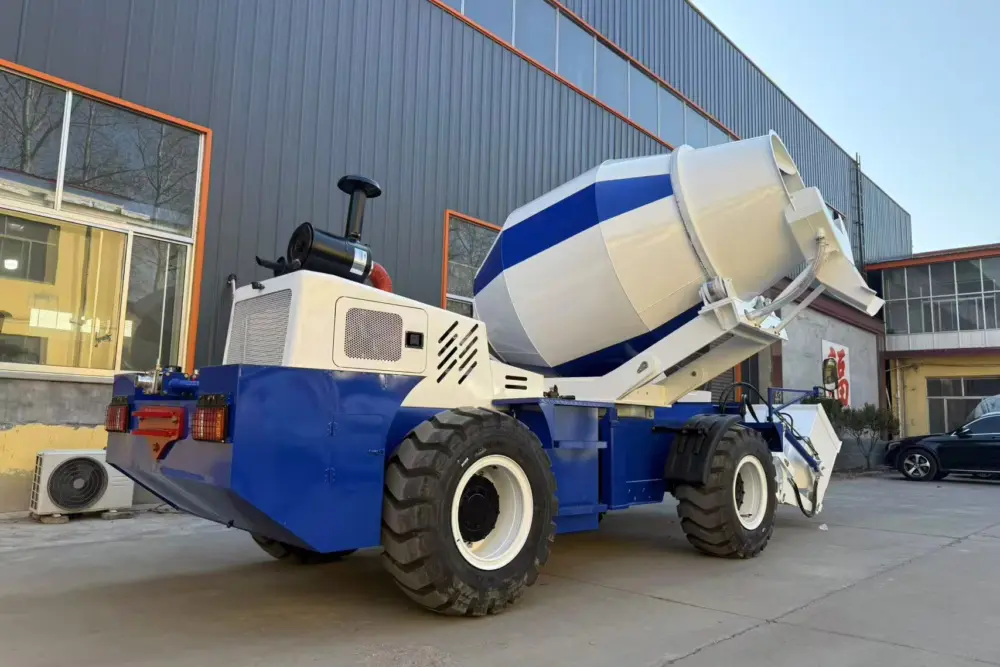
Record minutes for each part of the cycle. Add loading, water, mixing, travel, discharge, return and routine non-producing time. Divide 60 by total cycle minutes to estimate theoretical hourly cycles, then check whether whole cycles fit the actual work period.
For example, a 20-minute complete cycle gives three theoretical cycles per hour. The output would be 4.8 m³/h for RB1600 or 7.5 m³/h for RB2500. These numbers illustrate the formula only; they are not measured Ray Bridge jobsite results.
Do Not Hide Utilisation Assumptions
An eight-hour shift rarely contains eight identical productive hours. Setup, material replenishment, travel changes, cleaning, inspections and other site events take time. State the productive-time assumption separately.
A transparent shift estimate might say: “2.5 m³ confirmed yield × 3 planned cycles/h × 6 productive hours = 45 m³ planned.” Every number can then be challenged or updated. Do not publish it as a machine guarantee.
Match Batch Size to Individual Pours
Daily volume is not the only question. A project may have several small placements. If the batch is larger than the practical pour, scheduling and concrete handling become more important. Record the volume and timing of each placement.
RB1600’s 1.6 m³ yield and RB2500’s 2.5 m³ yield create different batch-planning units. Select based on the structure and sequence, not only the largest daily total.
Check Material and Water Layout
The distance between stockpiles, water and pour points can dominate cycle time. Map the route and identify how materials are replenished. A machine specification cannot predict the effect of a poorly arranged site.
Concrete inputs and mix requirements are project responsibilities. Use approved materials and procedures, and follow the confirmed machine manual.
Include Access and Travel Constraints
RB1600 measures 6,750 × 2,350 × 2,450 mm and weighs 5,200 kg. RB2500 measures 6.8 × 2.3 × 2.9 m and weighs 6,900 kg. RB4000 measures 7,700 × 2,580 × 3,450 mm and weighs 8,300 kg.
Route width, clearance, turning area, surface and grade can limit cycle movement. Maximum speeds of 25 km/h, 35 km/h and 25 km/h respectively are not appropriate substitutes for measured site travel time.
Account for Discharge Position
Repositioning can add time. RB2500 lists 270° discharge rotation. RB4000 lists 270° drum swing and hydraulic chute-angle control. Confirm the placement layout and supplied discharge equipment rather than assuming a feature eliminates every move.
Use a Site Trial to Replace Assumptions
Once the exact machine and site are available, record several complete cycles under representative conditions. Separate unusual delays from recurring tasks. Update the planning model with the median or another deliberately selected measure and retain the observations.
A site trial also helps reveal whether material staging, access or placement—not mixing—is the main constraint.
Output Worksheet
- Enter confirmed concrete yield.
- List each cycle activity and minutes.
- Calculate complete cycles per hour.
- Apply realistic productive time.
- Check individual pour sizes.
- Record access and discharge delays.
- Run low, expected and high scenarios.
- Replace assumptions with observed data.
Low, Expected and High Scenarios
Use three cases instead of one exact-looking forecast. The low case includes longer cycles and fewer productive hours. The expected case uses the best current site information. The high case must not exceed supported machine and operating assumptions.
Show the range to project planners. This is more useful than advertising a single daily output that ignores jobsite variation.
Questions to Ask Before Using a Supplier Output Claim
- Does capacity mean yield or drum volume?
- Which exact model and configuration was tested?
- What activities are included in cycle time?
- What travel distance and site layout were used?
- How many productive hours are assumed?
- Is the number a maximum, average or guarantee?
- Is there model-specific evidence?
Use the Current Product Data
The RB1600 and RB2500 pages provide confirmed yield and listed batch rate. The RB4000 page clearly marks yield TBD. Preserve those labels in every calculation.
Worked Planning Scenarios
Scenario A: short cycles
Assume, for illustration, that the complete observed cycle is 18 minutes. That permits three complete cycles within an hour, with time remaining that should not automatically be counted as a fourth batch. RB1600 planning output would be 4.8 m³ for those three cycles; RB2500 would be 7.5 m³.
Scenario B: longer travel
If the cycle rises to 30 minutes because of travel and discharge, the plan becomes two batches per hour: 3.2 m³ for RB1600 or 5 m³ for RB2500. The machines have not changed; the site workflow has.
These examples show why daily output should be a range. They are arithmetic demonstrations, not performance records or customer cases.
Check Units and Rounding
Keep batch yield in cubic metres and cycle time in minutes. Calculate with unrounded inputs where possible, then state how the displayed number was rounded. Do not combine cubic yards and cubic metres without a documented conversion.
When a partial cycle does not fit the working period, do not count it as completed output. For scheduling, it is usually clearer to count whole batches and then review whether the final placement requires a smaller planned batch.
Separate Machine Time from Project Time
Concrete placement, finishing, sampling and curing can control the project even when the mixer is ready. Record these activities separately. Improving machine cycle time does not necessarily increase accepted concrete output if the placement team or structure cannot receive it.
Document the Result After Work Begins
Keep a simple batch log with date, model, confirmed batch setting, start and finish times, travel minutes, discharge location and interruptions. Use it to improve planning, not to rewrite the product specification.
When sharing an output result, state the site conditions and number of observed cycles. A measured result from one layout should not be advertised as a universal hourly or daily capacity for every buyer.
If the observed value differs greatly from the plan, review material staging, route, placement and operating procedure before attributing the difference to one machine feature.
Avoid False Precision
An estimate such as 7.37 m³/h can look measured even when its cycle time is only an assumption. Round planning outputs appropriately and show the underlying yield, cycles and productive time. Use ranges when site conditions are uncertain, and label observed results separately from forecasts.
Frequently Asked Questions
How many cubic metres can a self-loading mixer produce per hour?
Multiply confirmed yield by realistic completed cycles. At the listed upper rate of four batches, RB1600 arithmetic is 6.4 m³/h and RB2500 is 10 m³/h, but actual output can be lower.
How many batches can a self-loading mixer make in a day?
Divide productive time by the complete observed or estimated cycle time. Do not multiply a maximum hourly rate by total shift hours without accounting for non-producing time.
What determines mixer cycle time?
Material layout, loading, water, mixing procedure, travel, discharge, return, cleaning and interruptions all contribute.
Can drum speed be used to calculate output?
No. Drum speed is not enough to determine yield, complete cycle time or site production.
What is the daily output of RB4000?
It is TBD because confirmed concrete yield and batch rate are not available in the current supplied specification.
How can I improve an output estimate?
Measure several complete cycles on the actual site, document productive time and update the calculation while keeping the confirmed yield unchanged.